Boiler Feedwater
Pump Analysis
NPSH analysis, deadhead diagnosis, recycle valve evaluation, and isometric drawings — resolving pump vibration and cavitation at an Iowa industrial facility with a 70-year-old steam system.
Pumps that hadn't run right in 70 years
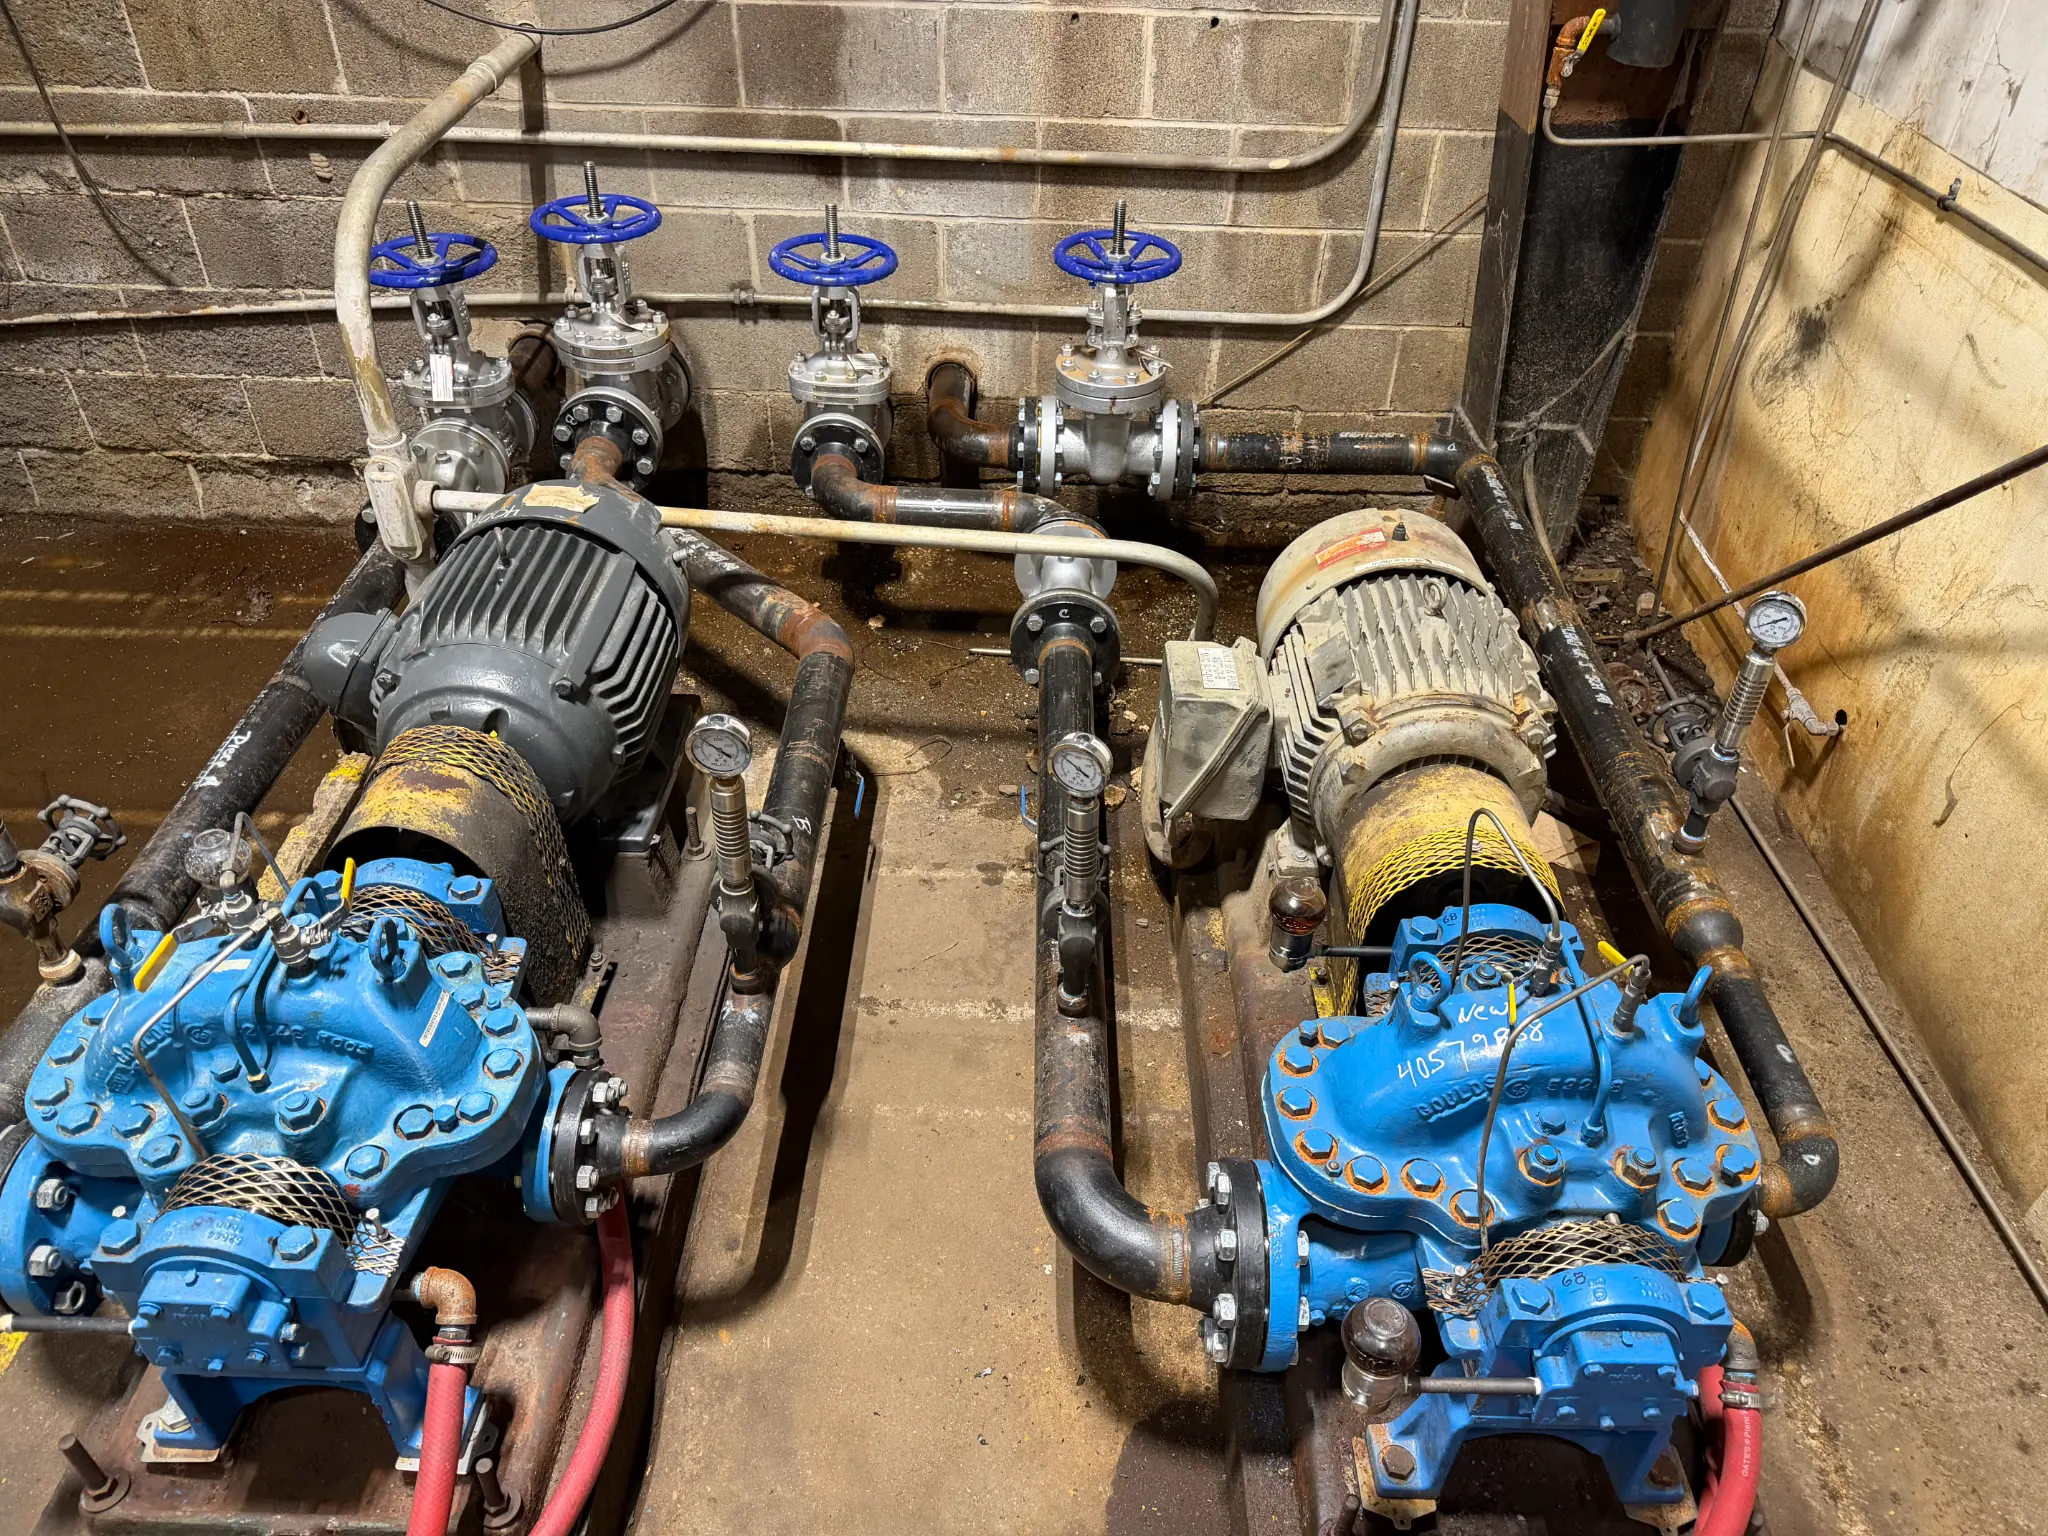
An Iowa industrial facility contacted Grey Engineering Enterprises about boiler feedwater pumps that were vibrating excessively and producing cavitation noise. The system had been in service for over 70 years, and the pumps had never performed to specification.
Our engineers conducted a full hydraulic investigation — analyzing the suction system from the deaerator, calculating available NPSH across the operating flow range, and identifying flow conditions that were driving the pumps into cavitation and deadhead operation.
The analysis identified the root causes and evaluated corrective options including minimum-flow recycle valve installation and piping reconfiguration. Isometric drawings were produced for the field modifications, and the engineering package was sealed by a licensed PE.
After implementation, the facility reported that the pumps were running smoother than at any point in the system's history — better than the original installation 70 years prior.
Request a Flow Analysis QuoteRoot cause to field-ready isometrics
Grey Engineering provided a complete hydraulic engineering package — from initial symptom diagnosis through corrective action design and isometric drawing production for field implementation.
Vibration & Noise Diagnosis
Field investigation of boiler feedwater pumps exhibiting excessive vibration and cavitation noise. Symptoms were traced to hydraulic root causes — not mechanical — requiring a full flow and NPSH analysis of the suction system before any corrective action could be specified.
NPSH Analysis — Deaerator Suction
Net Positive Suction Head (NPSH) analysis of the suction piping from the deaerator to the BFW pump inlets. Available NPSH (NPSHa) was calculated at multiple operating conditions and compared against the pump's required NPSH (NPSHr) to quantify the cavitation margin across the operating flow range.
Deadhead & Recycle Valve Evaluation
Flow analysis to identify deadheading conditions — operating scenarios where the pump was running against a closed or near-closed discharge, causing the pump to operate far left of its best efficiency point (BEP). Multiple corrective options were evaluated, including minimum-flow recycle valve sizing and piping reconfiguration.
System Curve & Pump Curve Analysis
System hydraulic model built to generate the system resistance curve across the full operating flow range. Pump curve overlay confirmed the operating point and identified flow regimes where cavitation and vibration were most likely to occur.
Isometric Drawings for Field Rerouting
Piping isometric drawings produced for the corrective piping modifications — rerouting and reconfiguration required to implement the engineering solution. Isometrics issued to the field for fabrication and installation, with dimensions, bill of materials, and weld callouts.
PE-Sealed Engineering Package
Complete engineering package — flow calculations, NPSH analysis, system curve, corrective action documentation, and isometric drawings — reviewed and sealed by a licensed Professional Engineer.
NPSH — the hidden cause of pump failure
Net Positive Suction Head (NPSH) is the margin between the energy available at the pump suction and the energy required to prevent the liquid from vaporizing inside the pump. When available NPSH (NPSHa) drops below the pump's required NPSH (NPSHr), the liquid flashes to vapor at the impeller eye — producing the characteristic cracking noise of cavitation and causing rapid impeller erosion.
In boiler feedwater systems, the suction source is typically a deaerator operating at elevated temperature and low pressure. This means the liquid is already near its boiling point before it reaches the pump — leaving very little NPSH margin. Any additional pressure drop in the suction piping, or any reduction in deaerator operating pressure, can push the system into cavitation.
Deadheading — running a pump with no flow through the discharge — is equally destructive. The pump recirculates internally, generating heat that raises the fluid temperature and further reduces NPSH margin, while the impeller operates at its maximum pressure rise with no cooling flow. Identifying and eliminating deadhead conditions is critical to long-term pump reliability.
- ✓NPSH calculation report — NPSHa vs NPSHr across full flow range
- ✓System curve and pump curve overlay analysis
- ✓Deadhead flow condition identification and documentation
- ✓Corrective option evaluation (recycle valve, piping reroute)
- ✓Piping isometric drawings for field modifications
- ✓Bill of materials for modified piping scope
- ✓PE-sealed engineering package for record
The pumps in the field
"The pumps had never run as smooth — better than they had from the original install 70 years ago."
After implementation of the engineered corrective measures, the facility reported that pump vibration and noise were eliminated. The BFW system operated reliably within its design envelope — a result the facility had not experienced since the original installation over seven decades prior.